Explore our premium range of custom corrugated mailers, magnetic rigid gift boxes, and recyclable apparel shipping solutions engineered for global fulfillment excellence.
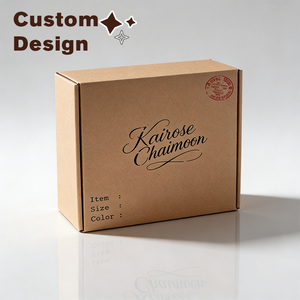
Heavy-duty E-flute/B-flute corrugated mailer engineered for garment shipping. High crush resistance with vibrant flexographic & offset custom printing.
Get Catalog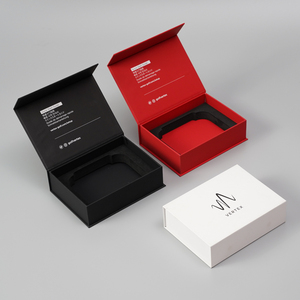
Luxury 1200gsm greyboard construction with invisible magnetic dual-closure. Custom laser-cut foam inserts for luxury apparel accessories and suits.
Get Catalog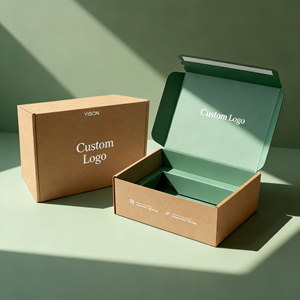
Frustration-free unboxing design featuring integrated self-adhesive sealing strips and dual tear-lines for effortless customer return logistics.
Get Catalog
Space-saving collapsible structure designed to minimize inbound warehouse storage costs while delivering ultra-premium retail shelf presentation.
Get Catalog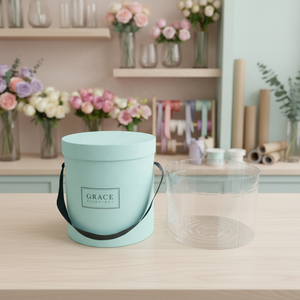
Cylindrical structural design crafted with water-resistant surface lamination. Tailor-made for headwear, boutique gowns, and luxury fashion items.
Get Catalog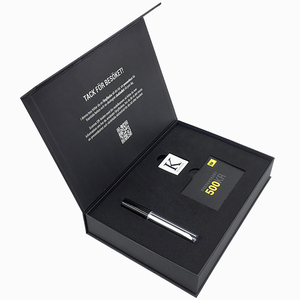
Deep matte black anti-scratch lamination with foil stamping options. Built specifically for high-impact influencer seedings and runway PR launches.
Get Catalog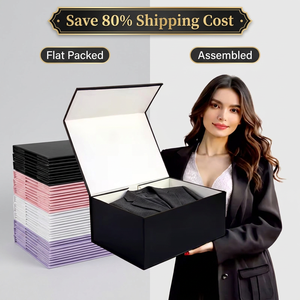
Features heavy-duty corner adhesive strips for instantaneous box setup. Provides structural integrity equal to traditional rigid boxes at 70% lower shipping volume.
Get Catalog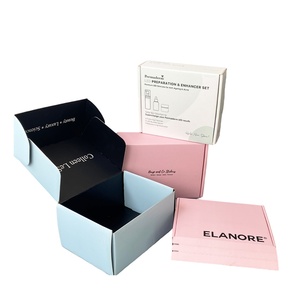
Engineered for direct-to-consumer (D2C) e-commerce brands. Double-wall side structure ensures zero crush damage during multi-stop courier transit.
Get CatalogIn the contemporary global retail environment, packaging is no longer merely a passive transport vessel; it is a highly regulated structural element that directly impacts compliance, brand equity, and supply chain efficiency. When sourcing apparel packaging for the European Union (EU) and international markets, securing CE Certified Apparel Packaging ensures that all paperboard, adhesives, coatings, and structural components adhere to strict safety, non-toxicity, and environmental mandates.
Information Gain Insight: While CE marking traditionally applies to machinery and medical devices, in the packaging domain, CE Compliance refers to strict adherence to EU Packaging and Packaging Waste Directives (94/62/EC), REACH Heavy Metals restrictions (EC 1907/2006), and EN 71-3 safety regulations for apparel packaging designed for infants and children.
Apparel items, particularly organic cotton garments, intimate wear, and children's apparel, are highly sensitive to chemical off-gassing and volatile organic compound (VOC) transfer from low-grade packaging materials. Our CE-compliant manufacturing process mandates:
To eliminate packaging failure during ocean freight, air parcel transit, and automated logistics sorting, our apparel packaging boards are engineered according to precise Edge Crush Test (ECT) and Bursting Strength (Mullen) benchmarks:
| Packaging Type | Material Specification | Caliper / Flute | ECT / Mullen Rating | Optimal Apparel Application |
|---|---|---|---|---|
| Corrugated E-Commerce Mailer | Uncoated Natural Kraft / White Kraft | E-Flute (1.6mm) | 32 ECT / 200 lbs/in² | T-shirts, Hoodies, Activewear, Denim |
| Heavy Duty Shipping Carton | Double-Wall Kraft Paperboard | BC-Flute (6.0mm) | 48 ECT / 275 lbs/in² | Bulk Garment Shipments, Outerwear Cases |
| Luxury Magnetic Apparel Box | 100% Recycled Rigid Greyboard | 1200 - 1800 GSM | Burst Pressure > 1.8 MPa | Tailored Suits, Evening Gowns, Luxury Leather |
| Foldable Folding Carton | Solid Bleached Sulfate (SBS) / CCNB | 18pt - 24pt Board | Stiffness > 15.0 mNm | Underwear Sets, Socks, Accessories |
The global apparel packaging market is undergoing a seismic shift driven by strict EU environmental legislation, consumer anti-plastic sentiment, and the rapid expansion of cross-border D2C e-commerce. Procurement directors must anticipate the following key trends to future-proof their supply chain:
Single-use polybags are being rapidly phased out in favor of 100% translucent glassine paper bags and recyclable corrugated structures. Mono-material packaging allows end-consumers to drop the entire packaging directly into domestic paper recycling streams without manual material segregation.
Modern apparel manufacturers are embedding ultra-thin RFID tags directly between the corrugated flutes of mailing boxes. This empowers automated warehouse scanning, real-time inventory tracking, anti-counterfeiting verification, and frictionless omnichannel customer returns.
Traditional poly-lamination is being replaced by aqueous barrier coatings. These bio-based water-repellent treatments protect apparel during wet shipping conditions while retaining 100% repulpability during municipal paper recycling operations.
As a leading global packaging manufacturer with primary US operations in West Chicago, IL and integrated production lines across Guangzhou, London, and Dubai, we bridge the gap between low-cost manufacturing and high-precision quality control.
Unlike traditional packaging mills requiring 5,000+ unit minimums, we accommodate growing apparel brands, boutique fashion houses, and promotional product drops with orders starting at just 50 units.
We source 100% FSC-certified virgin and post-consumer recycled (PCR) paper fibers. All printing is executed using non-toxic soy-based and vegetable-based inks delivering crisp CMYK + Pantone color accuracy.
From our West Chicago facility, we offer direct packaging kitting, pick-and-pack warehousing, and dropshipping services to streamline your end-to-end garment fulfillment workflow.
